
 English
 Chinese
1. Diameter tolerance
The diameter tolerance for circular optics provides an acceptable range of diameter values. This production specification will vary depending on the skill level and capabilities of certain optical processing companies that manufacture optical products. While the diameter tolerance does not have any effect on the optical performance of the optical product itself, it is a very important mechanical tolerance that you must consider if you are going to mount the optical product on any kind of holder. For example, if the diameter of a lens deviates from its nominal value, it is possible to deviate the mechanical axis from the optical axis in a mounted assembly, resulting in decentered light (Figure 1). Generally, the production tolerance for diameter is: +0.00/-0.10 mm for normal quality, +0.00/-0.050 mm for precision quality, and +0.000/-0.010 mm for high quality.
2. Center thickness tolerance
The central thickness of an optical element (most typically a lens), which measures the thickness of the material in the central portion of the optical element. The central thickness is measured by the mechanical axis of the lens, which is defined as the axis between the outer edges of the lens. Variations in the center thickness of a lens can affect optical performance because the center thickness and its radius of curvature determine the optical path length of light rays through the lens. Generally, production tolerances for center thickness are: +/-0.20 mm for normal quality, +/-0.050 mm for precision quality, and +/-0.010 mm for high quality.
3. Radius of curvature
The radius of curvature is the distance between the vertex of the optic and the center of curvature. The radius can be positive, zero, or negative, depending on whether the surface is convex, flat, or concave. Knowing the value of the radius of curvature can determine the optical path length of the light rays through the lens or mirror, and also plays an important role in determining the surface power. The production tolerance for the radius of curvature is typically +/-0.5, but can be as low as +/-0.1% for precision applications, or +/-0.01% where extremely high quality is required.
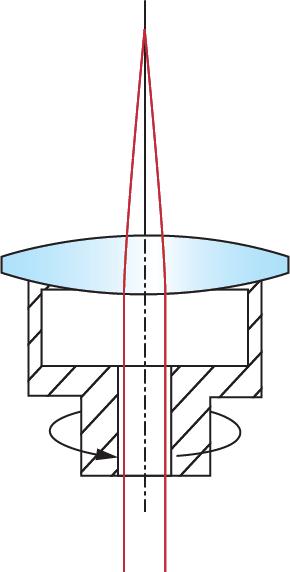
The center of the lens, also known as centripetal or centrifugal, is specified in terms of beam deviation δ (Equation 1). Once the beam deviation is given, the wedge angle W can be calculated by a simple relationship (Equation 2). The eccentricity of a lens is the distance that the mechanical axis is physically offset from the optical axis. The mechanical axis of a lens is simply the geometric axis of the lens, defined by its outer cylinder. The optical axis of the lens is defined by the optical surfaces, which are lines connecting the centers of curvature of each surface. To perform a centripetal test, place the lens in a teacup and apply pressure to it. The pressure applied to the lens is automatically focused on the center of curvature of the first surface in the center of the cup, and this center is also aligned with the axis of rotation (Figure 2). Parallel light incident along this axis of rotation will pass through the lens to the focal point in the back focal plane. As the lens rotates as the teacup rotates, any centrifugality in the lens will disperse the focused beam and create a circular trajectory of radius Δ at the back focal plane.
4. Parallelism
Parallelism describes the relationship between two parallel surfaces. It is useful when specifying components such as windows and polarizers, where parallel surfaces are ideal planes to improve system performance because they minimize distortion that would otherwise degrade image or light quality. Typically, this tolerance ranges from 5 arc minutes up to a few arc seconds.
5. Angle tolerance
In components such as prisms and beamsplitters, the angle created between the surfaces has a significant impact on the performance of the optical product. Angular tolerances are usually measured using collimated telescope assemblies, whose light source systems emit parallel light. The collimating telescope will rotate around the surface of the optical product until the resulting Fresnel is reflected back to the surface, creating a spot of light on top of the detected surface. This verifies that the parallel beam is exactly perpendicular to the surface. The entire collimating telescope assembly is then rotated around the optical product to the next optical surface, and the process is repeated. Figure 3 shows a generic collimating telescope setup for measuring angular tolerances. The angular difference between the two measurement locations can be used to calculate the tolerance of the two optical surfaces. The angular tolerance can range from a few arc minutes down to a few arc seconds.
6. Chamfer
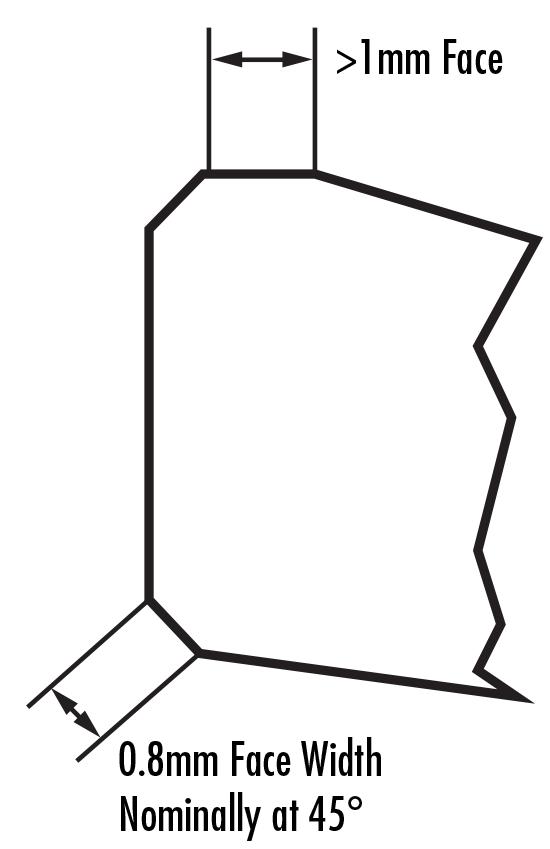
Glass corners are very fragile, so it is important to protect them when handling or installing components. The most common way to protect these glass corners is to chamfer these edges. The chamfer acts as a protective groove to prevent chipping at the edges. They are defined by the width and angle of their surfaces. The most common cut angle for chamfers is 45°, and this surface width is determined by the diameter of the optical product. Optical products with a diameter of less than 3.00mm (such as microlenses or microprisms) generally do not need to be chamfered because edge chipping is likely to occur during the cutting process. It is worth noting that for very small radii of curvature, for example, when the diameter of the lens is greater than or equal to 0.85 x radii of curvature, chamfering is not necessary because of the large angle formed between the lens surface and the edge. For all other diameters, Table 1 provides the maximum surface widths.
7. Clear aperture
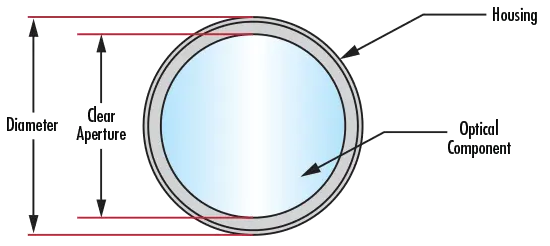
Clear aperture refers to the diameter of an optical element or the size of an optical element that must meet various specifications. With the exception of clear aperture, manufacturers cannot ensure that optical products meet specified specifications. Due to production constraints, it is practically impossible to produce a clear aperture that is exactly equal to the diameter or length times the width of the optical product. Table 2 shows typical clear apertures for lenses.
8. Surface Quality
The quality of the optical surface is used to measure the surface characteristics of optical products, and covers some defects such as scratches and pits. Most of these surface imperfections are purely cosmetic and do not have a large impact on system performance, although they may cause a small dip in system throughput and more subtle scattering of scattered light. However, some surfaces are more sensitive to these effects, such as: (1) surfaces at the image plane, as these imperfections can create focus, and (2) surfaces with high power levels, as these imperfections can increase energy absorption and destroy optical products . The most commonly used specification for surface quality is the scratch and pit specification specified by MIL-PRF-13830B. The scratch name is determined by comparing scratches on the surface to a series of standard scratches provided under controlled lighting conditions. So the scratch name doesn’t describe its actual scratch, but compares it to a standard scratch according to MIL specs. However, the pit name is directly related to the point or pit on the surface. The pit name is calculated by dividing the pit diameter in microns by 10, generally a scratch pit gauge between 80 and 50 will be considered standard quality, between 60 and 40 is exact mass, and at 20 A value between 10 and 10 is considered high precision quality.
9. surface flatness
p>Surface flatness is a type of specification that measures the accuracy of a surface, it is used to measure the deviation of planes such as mirrors, windows, prisms or flat mirrors. You can measure this deviation using an optical flat, which is a high-quality, high-precision reference plane used to compare the smoothness of specimens. When the plane of the optical product being tested is placed against the optical flat, streaks appear, the shape of which is indicative of the surface smoothness of the optical product being tested. If the fringes are equally spaced and are parallel straight lines, then the optical surface being inspected is at least as flat as the reference optical flat. If the fringes are curved, the number of fringes between two dashed lines (one tangent to the midpoint of the fringe and the other dashed across the endpoints of the same fringe) would indicate a smoothness error. Deviations from smoothness are usually measured in ripple values (λ), which are made up of test sources at multiple wavelengths. A fringe corresponds to ½ wavelength. A smoothness of 1λ indicates a general quality level; a smoothness of λ/4 indicates an accurate quality level; a smoothness of λ/20 indicates a high-precision quality level.
10. Aperture amount
F-number is a type of specification that measures the accuracy of a surface, and it applies to curved optical surfaces or surfaces with power. A test of f-stop is similar to a flatness test, comparing a curved surface to a reference surface with a highly calibrated radius of curvature. Using the same interference principle created by the voids of these two surfaces, the fringe interference pattern is used to represent the deviation of the test surface from the reference surface (Figure 6). The deviation from the reference will produce a series of circular rings called Newton’s rings . The more rings present, the greater the deviation. The number of dark or bright rings, rather than the sum of both dark and bright rings, is equal to 2 times the wavelength error.
11. Irregularity
Irregularity is a type of specification that measures the accuracy of a surface and describes the deviation between the shape of the surface and the shape of a reference surface. Irregularity is measured in the same way as f-stop. Regularity refers to the spherical, circular fringes formed by comparing the test surface to the reference surface. When the f-number of the surface exceeds 5 fringes, it will be difficult to detect small irregularities of less than 1 fringe. Therefore, it is common practice to specify the f-number to irregularity ratio of the surface to be approximately 5:1.
Surface finishing, also known as surface roughness, is used to measure some small irregularities on a surface. They are usually undesirable consequences of the polishing process. Rough surfaces tend to be more wear resistant than smooth surfaces, and may not be suitable for some applications, especially in applications using lasers or hot environments, because of the potential for microscopic cracks or imperfections at the nucleation sites. Production tolerances for surface finishing are average quality at 50Å RMS, exact quality at 20Å RMS, and high quality at 5Å RMS.


